Industry
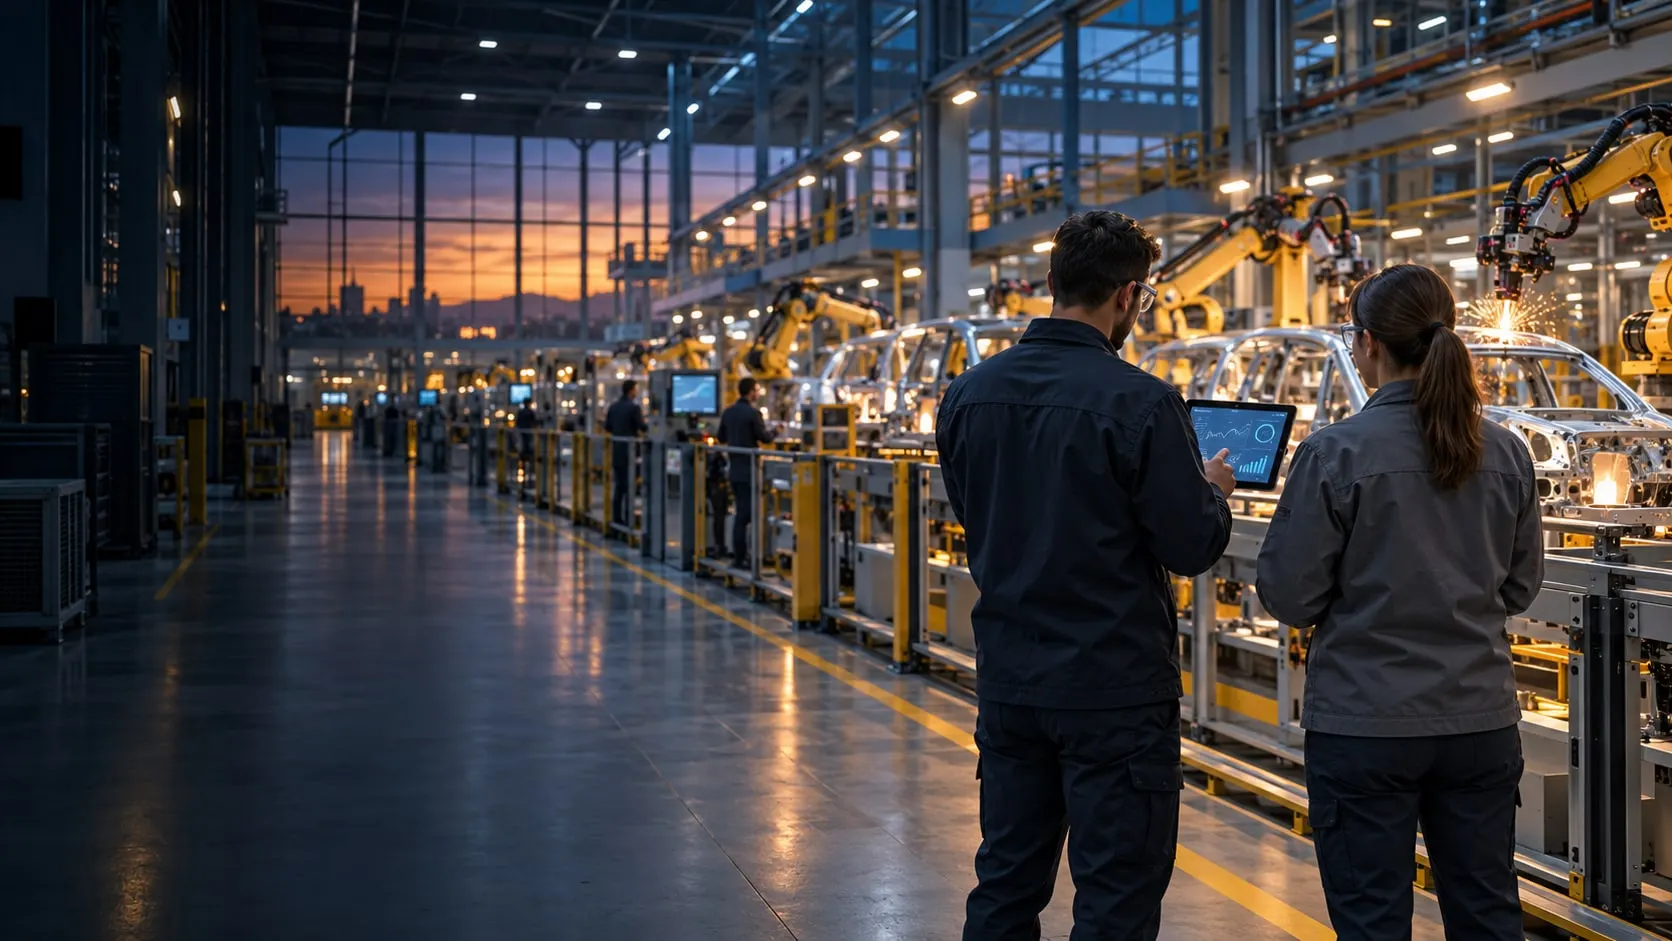
Production tracking and test data for appliance and electronics assembly lines
We combine data from assembly stations, end-of-line testers and poka-yoke checks under each product's serial number.
Our clients
- Siemens
- Anadolu Isuzu
- BSH
- Tofaş
- Toyotetsu
- Martur
- Turkcell
- Vodafone
- Doğadan
- Pakmaya
- Bross
- Abdi İbrahim
- Nobel İlaç
- Plastimak
- Dalgıç Kalıp
- Barbaros Motor
- Magneti Marelli
- Rözmaş
- Sanel
Appliance and electronics lines run at a high pace, and a delay at one station breaks the takt of the whole line. On the quality side, you must show that every unit passed end-of-line testing, received the right part and had its screws driven to the right torque.
VOLSOFT reads data from station PLCs, torque and screwdriving systems, barcode readers and end-of-line testers without touching control logic. Each record is tied to the product serial number and the work order.
Line balance, station-level downtime, test reject reasons and repair loops then show up in one data layer, and when a field failure comes back, the unit's assembly and test history is found by serial number. Every project runs on Proxus.
What we deliver
Appliances and electronics
-
Station-level takt and downtime
Cycle time, waiting and stoppages are measured for each station, so line imbalance and the bottleneck station are visible in the data.
-
End-of-line test records
Results and measured values from electrical safety, functional, leak and performance tests are stored with the serial number.
-
Poka-yoke and part verification
Critical parts scanned at the station are checked against the product's bill of materials, and a mismatch is shown as a warning at the station.
-
Torque and screwdriving data
Torque and angle values are read from screwdriving systems and written to the unit's record.
-
Repair loops and reject analysis
Repair actions on failed units and their retest results are tracked, and reject reasons are reported as a Pareto.
Processes we work on
Where the data starts in appliances and electronics
- Assembly lines and stations
- End-of-line functional and safety tests
- Leak testing and refrigerant charging
- Screwdriving and torque control
- Poka-yoke and part verification
- SMT and PCB assembly
- Polyurethane foam injection
- Sheet metal forming and painting
- Packaging and palletizing
How a project runs
From discovery to live, step by step
- 01
Line and station analysis
Station PLCs, testers, screwdriving systems and barcode points are reviewed on site, and we map where the serial number is created and how it travels down the line.
- 02
Data model and pilot line
A shared data model for station, test and product records is built and put live on one line.
- 03
Tester and ERP integration
End-of-line test results are connected, along with ERP work orders, bills of materials and production confirmations.
- 04
Rollout and training
Further lines are added on the same model, and production, quality and process engineering teams are trained.
Built on Proxus
Proxus publishes station and tester data in a Unified Namespace organized by line, station and product, so MES, ERP and quality systems read from the same source.
Proxus is the industrial data platform built by the VOLSOFT team.
Frequently asked questions
Common questions
How is serial number traceability achieved on an assembly line?
A serial number is assigned at the start of the line and read at every station, so each station's data is recorded against it. Critical part barcodes, torque values and test results are added to the same record. The unit's assembly and test history can then be queried by serial number.
Can data from end-of-line testers be collected?
Yes. Measured values and pass/fail results are taken from the testers' result files, databases or communication interfaces and matched with the product serial number.
Can poka-yoke checks be done in software?
Checks such as part verification can run in the software layer: the scanned barcode is compared with the bill of materials and a mismatch is shown at the station. Physical interlocks that stop the line stay in the existing automation and are planned with the plant's automation team.
How is OEE calculated on an assembly line?
On assembly lines OEE is usually calculated per line from takt time and planned production time. Station-level cycle and downtime data then show which station the losses come from.
How long does a project take in an appliance or electronics plant?
It depends on the number of lines and stations, the variety of testers and the ERP integration. Projects usually start with a pilot on one line, and the scope is set during the discovery call.
Related pages
Often looked at together
- Solution OEE Software OEE software fed by PLC and CNC data, with downtime reasons, work orders and ERP sync. Explore →
- Solution Unified Namespace (UNS) One namespace for plant data: ISA-95 topic structure, naming rules, MQTT and governance. Explore →
- Service MES and OEE Implementation Production tracking with automatic OEE, downtime, work orders and shift reports from machine data. Explore →
- Service Machine Data Collection Read-only production data collection from PLCs, CNCs and robots, with control logic left untouched. Explore →
- Service ERP–MES Integration Work-order and production feedback integration with SAP, Dynamics and other ERPs. Explore →

Next step
Let’s turn your goal into a clear engineering scope.
Tell us about your plant, your machines and your goal. An integration engineer will set up a discovery call with you.



